Engineering Strategy for Robotic Bridge Truss Fabrication
The fabrication of bridge trusses represents one of the most demanding applications in structural engineering due to the requirement for high fatigue resistance and the management of massive weld volumes. Traditional welding methods often rely on wide-angle V-groove preparations, which necessitate extensive filler metal deposits and result in significant thermal distortion. By pivoting to a Robotic Welding Cell optimized for Narrow Gap (NG) configurations, industrial operations can achieve higher weld quality with a fraction of the material throughput.
The transition to robotic MAG welding in a narrow gap setting involves reducing the bevel angle to between 1 and 5 degrees. This geometry significantly lowers the cross-sectional area of the joint, requiring fewer passes to achieve full penetration. However, the narrowness of the groove introduces technical challenges in gas shielding and arc stability that only the precision of a robotic arm can reliably navigate.
Narrow Gap MAG Process Parameters
In a robotic cell, the Metal Active Gas (MAG) process is refined through pulsed-arc waveforms to control the droplet transfer and minimize spatter. for Bridge Trusses, which often utilize high-strength low-alloy (HSLA) steels, maintaining a consistent Heat Input is critical to preserving the mechanical properties of the base metal.
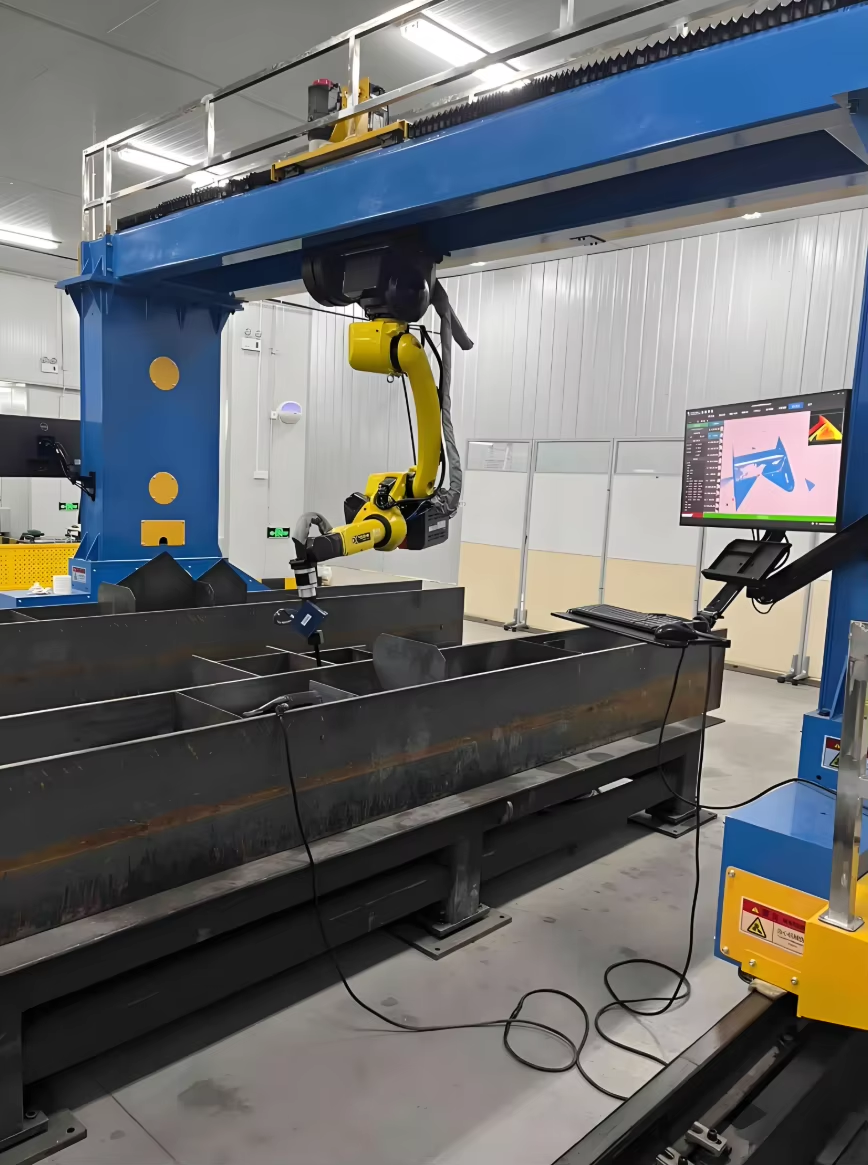
The robot utilizes advanced seam tracking—typically through through-arc sensing or tactile probing—to ensure the torch remains centered within the narrow groove. Because the clearance between the contact tip and the sidewall is minimal, the system must execute a precise oscillation pattern. This ensures sidewall fusion without undercutting. The use of a specialized long-reach torch with a narrowed gas nozzle is essential to provide adequate laminar flow of the shielding gas (typically an Argon/CO2 mix) at depths exceeding 50mm.
System Maintenance and Reliability Protocols
High-uptime environments require a shift from reactive to Preventative Maintenance. In a robotic MAG cell, the wire delivery system is the most frequent point of failure. The mechanical components, including the drive rolls, the conduit liner, and the contact tip, must be inspected on a strictly metered schedule based on “Arc-On” hours rather than calendar days.
Contact Tip and Diffuser Lifecycle
In narrow gap welding, the contact tip is subjected to intense radiant heat from the constrained arc environment. Micro-arcing within the tip can lead to “keyholing,” which destabilizes the arc and causes erratic wire delivery. Standard operating procedures should dictate contact tip replacement every 4 to 8 hours of continuous welding, depending on the current density. Utilizing high-quality chrome-zirconium copper tips can extend this lifecycle by approximately 25% compared to standard E-Cu tips.
Torch Calibration and TCP Alignment
The Tool Center Point (TCP) is the mathematical coordinate of the wire tip relative to the robot flange. In heavy truss fabrication, minor collisions or thermal expansion can shift the TCP. An automated TCP check station should be integrated into the cell, allowing the robot to verify its alignment every 10 cycles. If the deviation exceeds 0.5mm, the system should trigger an automatic recalibration to prevent lack-of-fusion defects in the narrow gap.
Labor ROI and Economic Impact Analysis
The primary driver for implementing a robotic welding cell is the decoupling of throughput from labor scarcity. Bridge truss welding is physically taxing and requires Level III certified welders. By automating the MAG process, the role of the human worker shifts from a manual operator to a Process Technician.
When calculating ROI, the engineer must look beyond the hourly wage. The “Arc-On” time for a manual welder in a heavy shop typically ranges from 20% to 30% due to fatigue, setup, and repositioning. A robotic cell can maintain an Arc-On time of 75% to 85%. In a narrow gap application, the savings are compounded. Because the narrow gap requires up to 50% less filler metal than a standard V-groove, the robot finishes the joint faster and uses significantly less consumable material.
Quantifying Throughput Gains
For a standard 100-foot bridge truss segment, a manual welding team might require 120 man-hours for completion, including cleaning and rework. A robotic cell can reduce this to 40 hours. This 3x increase in capacity allows for shorter project lead times and lower overhead per ton of fabricated steel.
Reduction in Non-Destructive Testing (NDT) Failures
Rework is the “hidden killer” of profitability in structural steel. Manual welding is prone to inclusions and porosity, especially during the long hours required for thick-plate joints. Robotic systems provide a digital record of every weld parameter, including voltage, current, and travel speed. This level of process control results in a 95%+ first-pass success rate for ultrasonic or radiographic testing, virtually eliminating the costs associated with gouging out and repairing defective welds.
Integration of Power Source Intelligence
Modern robotic power sources provide real-time data logging. For bridge truss fabrication, this data is used to ensure compliance with AWS D1.5 (Bridge Welding Code). By monitoring the “heat input per inch,” the industrial engineer can verify that the cooling rates of the weld metal remain within specified limits to prevent hydrogen-induced cracking.
Data-Driven Optimization
By analyzing the data harvested from the welding cell, engineers can identify bottlenecks in the jigging and fixture phase. If the robot is waiting for parts to be loaded, the ROI on the machine is diminished. Therefore, the implementation of a robotic cell often necessitates a redesign of the shop floor layout to include dual-zone workstations, where the robot welds in Zone A while technicians load the next truss segment in Zone B.
Final System Evaluation
The adoption of robotic narrow gap MAG welding is not merely a hardware upgrade but a fundamental shift in fabrication logic. The synergy between reduced weld volume and automated consistency creates a competitive advantage in the heavy infrastructure sector. While the initial capital expenditure (CAPEX) for a robotic cell is high, the reduction in consumables, the stabilization of labor costs, and the drastic improvement in quality metrics ensure a payback period typically within 18 to 24 months in a high-volume bridge shop.
-


LT240S tube laser cutting machine
-
LT120S tube laser cutting machine
-
Sale

Tank Fillet Welding Machine
Original price was: $1,000.00.$900.00Current price is: $900.00. -
Sale

MAK100 tube laser cutting machine
Original price was: $5,500.00.$5,000.00Current price is: $5,000.00. -

portable plasma air cutting machine
$1,200.00 -

2in1 fiber laser cutting machine
-

Air cooling Laser welding machine
-

HF h beam laser cutting machine
-

LT240 laser cutting machine
-

Laser welding machine
-


Cobot Welding Station
-

Gantry welding robot solution
-

Tracked Wheeled AGV Welding robot
-

LFH6020 Fiber laser cutting machine
-
LFP6020
-

robotic welidng machine
Advanced Fiber Laser Tube Processing Technology
Our CNC Fiber Laser Tube Cutting systems revolutionize metal fabrication by integrating high-precision cutting, punching, and profiling into a single automated workflow. Designed for versatility, this technology handles a wide array of profiles including Round, Square, Rectangular, and Oval tubes, as well as complex L-shaped and U-shaped channels.
- Precision Punching: High-speed hole punching with micron-level accuracy, eliminating the need for mechanical drilling or die-stamping.
- Complex Profiling: Advanced 3D pathing allows for intricate interlocking joints and specialized notch cuts, ideal for structural frames.
- High Material Efficiency: Intelligent nesting software minimizes scrap, reducing raw material costs across large production runs.
- Clean Finish: Delivers oxide-free, burr-free edges that require zero secondary grinding before welding.

Seamlessly processing multiple profiles with consistent precision.
Global Delivery & Logistics



From our high-tech manufacturing facility directly to your global site. PCL WeldCut ensures secure packaging, professional handling, and reliable international logistics to safeguard your equipment throughout the entire journey.