Beam Processing Center with Arc Voltage Control for for Steel Structure
In this article
- Optimizing Structural Steel Fabrication via Plasma Beam Processing
- The Technical Role of Arc Voltage Control (AVC)
- Maintaining Optimal Standoff Distance
- Impact on Consumable Longevity
- Precision in Complex Intersection Geometries
- Low Maintenance Requirements for H-Beam Processing
- Multi-Axis Beveling for Weld Preparation
- Robotic Integration and Bevel Accuracy
- Enhancing Downstream Efficiency
- Conclusion
Optimizing Structural Steel Fabrication via Plasma Beam Processing
In the current landscape of heavy industrial construction, the transition from manual layout and mechanical drilling to automated Beam Processing Centers has redefined throughput expectations. For structural steel applications involving H-beams, channels, and hollow sections, Plasma Cutting accuracy is the primary driver of assembly efficiency. Unlike mechanical methods, plasma systems offer the agility to handle complex geometries while maintaining the structural integrity required for high-load environments.
The efficiency of a beam processing center is not merely a function of movement speed but of the stabilization of the cutting arc. High-definition plasma systems, when integrated with robust CNC controls, allow for the execution of intricate bolt holes, copes, and notches without the tool wear associated with physical contact machining. This engineering approach focuses on the synchronization of motion control and plasma dynamics to eliminate secondary grinding operations.
The Technical Role of Arc Voltage Control (AVC)
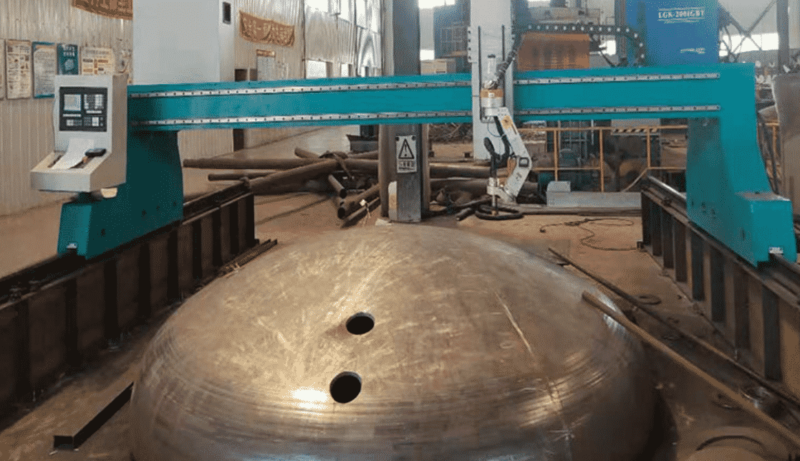
At the core of high-performance plasma beam processing lies Arc Voltage Control (AVC). This technology functions as a closed-loop feedback system that monitors the electrical potential between the plasma torch electrode and the workpiece. In structural steel fabrication, beams are rarely perfectly flat or straight; flange warping, web bowing, and mill tolerances are inherent variables that can compromise cut quality if not addressed in real-time.
Maintaining Optimal Standoff Distance
AVC systems work by measuring the voltage of the plasma arc, which is directly proportional to the arc length. As the distance between the torch and the steel beam increases, the voltage rises. Conversely, as the torch moves closer, the voltage drops. The CNC controller interprets these fluctuations and adjusts the Z-axis height instantaneously to maintain a constant standoff distance. This constant height is critical for ensuring a uniform kerf width and preventing dross accumulation on the underside of the flange.
Impact on Consumable Longevity
From an industrial engineering perspective, the stabilization provided by AVC significantly extends the life of nozzles and electrodes. By preventing “torch dives”—where the torch makes physical contact with the workpiece due to beam irregularities—the system avoids catastrophic consumable failure and minimizes downtime. Consistent arc voltage ensures that the plasma gas flow and current density remain within designed parameters, providing a stable thermal environment for the cutting process.
Precision in Complex Intersection Geometries
The structural integrity of a steel frame depends heavily on the fit-up of its components. Structural steel fabrication requires high-precision intersections where beams meet at various angles. Plasma beam processing centers utilize multi-axis robotic arms or specialized gantry systems to navigate the three-dimensional profile of an H-beam, executing cope cuts and block-outs that would be nearly impossible with traditional sawing.
Managing Thermal Influence and Kerf Compensation
One of the challenges in plasma cutting is the management of the heat-affected zone (HAZ). Modern beam processing centers utilize advanced algorithms to adjust cutting speeds and gas pressures based on the thickness of the material being penetrated. When cutting through a thick flange versus a thinner web, the system must modulate its parameters to maintain intersection accuracy. Precision is further enhanced through kerf compensation software, which accounts for the width of the plasma arc to ensure that the finished dimensions of the cutouts match the CAD/CAM specifications exactly.
H-Beam Web and Flange Synchronization
Accurate intersections require the system to transition seamlessly between the web and the flange. This requires high-speed communication between the AVC and the motion controller. As the torch rounds the radius of the beam (the “toe”), the arc voltage can fluctuate wildly. Advanced beam processors use look-ahead logic to anticipate these geometry changes, slowing the feed rate and adjusting the voltage setpoint to prevent “rounding” of corners and ensuring that bolt holes remain perfectly cylindrical rather than tapered.
Low Maintenance Requirements for H-Beam Processing
One of the most compelling arguments for adopting plasma-based beam processing is the reduction in mechanical maintenance. Traditional drilling and sawing lines involve numerous moving parts, coolant systems, and perishable tools that require frequent replacement and calibration. In contrast, plasma cutting accuracy is achieved through an electro-thermal process that involves no physical force against the workpiece.
Eliminating Mechanical Stress
Because plasma cutting is a non-contact process, there is no lateral force exerted on the beam or the machine frame. This eliminates the need for the massive clamping systems and heavy-duty foundations required by high-speed drills. The lack of mechanical vibration reduces the wear and tear on bearings, rails, and drive motors, leading to a longer Mean Time Between Failures (MTBF) for the entire processing center.
Simplified Waste Management
Plasma systems also simplify the shop environment. Unlike mechanical processing, which produces sharp metal chips and requires liters of cutting fluid that must be recycled or disposed of, plasma cutting produces fine dust and dross. Most modern beam processing centers are equipped with integrated downdraft tables or specialized filtration units that capture these particulates, keeping the workspace cleaner and reducing the maintenance burden on the facility’s air handling systems.
Multi-Axis Beveling for Weld Preparation
The final critical advantage of plasma beam processing centers is their ability to perform weld preparation directly on the processing line. In structural steel, most moment connections and heavy-duty joints require beveled edges (V, Y, or K-cuts) to ensure full penetration welds. Manually grinding these bevels is labor-intensive and prone to human error.
Robotic Integration and Bevel Accuracy
By utilizing a 5-axis or 6-axis robotic plasma head, the beam processing center can tilt the torch to the precise angle required by the welding specification. The AVC remains active during this process, though the voltage-to-distance calculation must be adjusted for the angle of the torch. This allows for the creation of consistent bevels across the entire length of a cope or a flange cut, ensuring that the fit-up on the job site is seamless.
Enhancing Downstream Efficiency
The ability to provide a weld-ready part directly from the processing center eliminates the need for a secondary beveling station. This streamlines the material flow through the shop and reduces the number of times a heavy beam must be handled by overhead cranes. When the plasma-cut beams arrive at the welding station, the clean, accurate bevels allow for faster setup and more consistent weld quality, directly contributing to the overall structural safety of the building or bridge being constructed.
Conclusion
The integration of Arc Voltage Control in plasma-based beam processing centers represents a significant leap forward for industrial steel fabrication. By prioritizing electrical arc stability, these systems deliver superior intersection accuracy and weld-ready components while significantly lowering the maintenance threshold compared to mechanical alternatives. For the industrial engineer, the result is a highly predictable, efficient, and scalable solution for the most demanding structural challenges.






