Beam Processing Center with Arc Voltage Control for for Steel Structure
In this article
Advanced Plasma Integration in Structural Steel Processing
In the current landscape of structural steel fabrication, the Beam Processing Center (BPC) serves as the primary engine for throughput and precision. Unlike traditional manual methods that rely on physical templates and handheld torches, modern BPCs utilize high-definition Plasma Cutting systems integrated with multi-axis robotics. This transition to automation is driven by the need for tighter tolerances and the reduction of labor-intensive secondary operations.
The core advantage of a plasma-based BPC lies in its ability to handle large-scale H-beams, channels, and hollow structural sections (HSS) with minimal downtime. For an industrial engineer, the focus is on optimizing the duty cycle and ensuring that the output meets stringent architectural and engineering specifications. By isolating the thermal cutting process to plasma, fabricators can achieve a balance between cutting speed and the quality of the heat-affected zone (HAZ), which is critical for maintaining the structural integrity of the steel.
The Mechanics of Arc Voltage Control (AVC)
Arc Voltage Control is the critical feedback loop that manages the distance between the plasma torch tip and the workpiece. In structural steel, material is rarely perfectly flat or straight. H-beams often exhibit web camber, flange tilt, or surface irregularities that can vary by several millimeters over the length of the section. If the torch remains at a fixed height, these variances lead to fluctuations in the arc length, which directly impacts the kerf width, dross accumulation, and cut angularity.
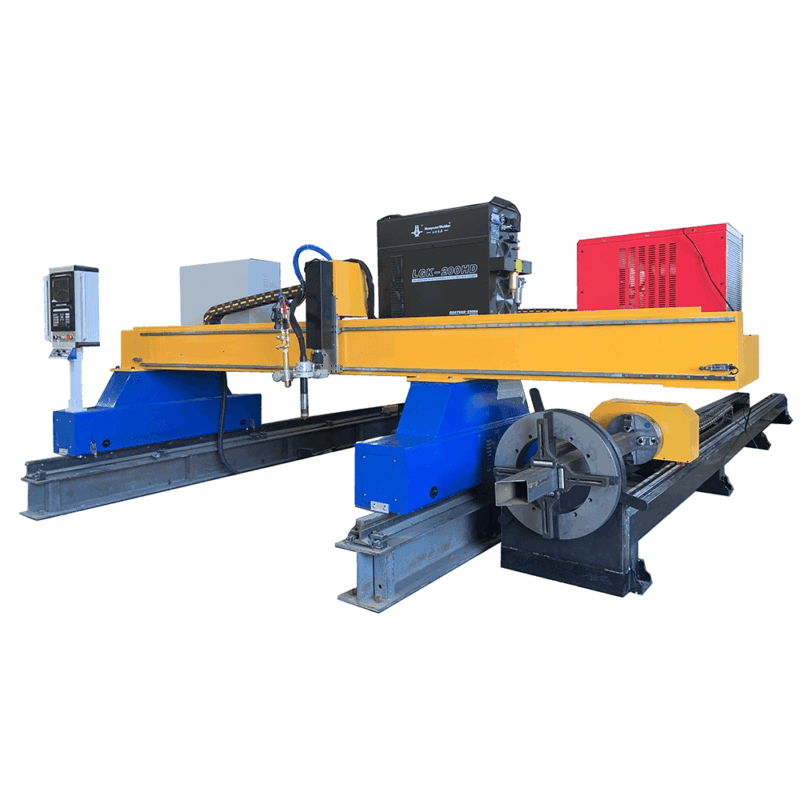
The AVC system functions by measuring the voltage of the plasma arc during the cutting process. Since the voltage is directly proportional to the length of the arc, the CNC system can adjust the Z-axis position in real-time to maintain a constant voltage setpoint. This ensures that the standoff distance remains uniform regardless of the beam’s physical deviations. For complex cuts, such as those passing through the radius of an H-beam, the AVC prevents torch collisions and ensures that the plasma stream remains at the optimal focal point for material penetration.
Ensuring Intersection Accuracy for Bolted Connections
One of the most significant challenges in steel fabrication is achieving high intersection accuracy. This refers to the precision required for bolt holes, copes, and notches where two structural members meet. In a Beam Processing Center, accuracy is a product of both the motion control system and the stability of the plasma arc.
When cutting bolt holes in the flange or web of a beam, the AVC ensures that the arc does not “dive” or “climb” as it encounters the heavy scale or surface oxidation common on hot-rolled steel. This stability results in holes that are perfectly cylindrical rather than tapered, meeting the requirements for high-strength bolted connections. Furthermore, the synchronization of the plasma system with the robotic arm allows for precise path planning. When the system executes a complex cope at the intersection of the flange and web, the AVC maintains the necessary arc characteristics to ensure the cut is clean and the dimensions are within the +/- 1mm tolerance required for modern BIM (Building Information Modeling) workflows.
Robotic Beveling and Weld Preparation Efficiency
Plasma cutting in a BPC is not limited to vertical cuts. The integration of 5-axis or 6-axis robotic heads enables the system to perform complex beveling. This is essential for preparing joints for Full Penetration (CJP) or Partial Penetration (PJP) welds. The ability to execute V-cuts, Y-cuts, and K-cuts directly on the beam processing line eliminates the need for manual grinding or secondary beveling stations.
During beveling, the Arc Voltage Control must be even more sophisticated. As the torch tilts to an angle, the effective thickness of the material increases, and the relationship between voltage and distance changes. Modern AVC algorithms compensate for these geometric shifts, ensuring that the bevel angle remains consistent across the entire length of the cut. This precision is vital for automated welding processes downstream, where fit-up gaps must be uniform to prevent welding defects like undercut or lack of fusion.
Low Maintenance Advantages for H-Beam Processing
From an operational perspective, the H-beam processing center utilizing plasma technology offers a significantly lower maintenance profile compared to mechanical cutting or older oxy-fuel systems. Plasma systems have fewer moving parts in the cutting head itself, and the primary consumables—nozzles, electrodes, and swirl rings—are designed for rapid replacement.
The robustness of plasma is particularly evident when dealing with the heavy mill scale found on H-beams. Unlike mechanical drills or saws that suffer tool wear and requires constant lubrication, plasma is a non-contact process. There is no mechanical force exerted on the beam, which reduces the wear and tear on the machine’s drive motors and linear guides. Furthermore, the AVC helps extend the life of consumables by preventing “snags” or “tip-ups” where the torch might hit the material. By maintaining the correct standoff distance, the AVC minimizes the back-spatter of molten metal into the nozzle, thereby increasing the number of pierces per electrode change.
Thermal Efficiency and Material Handling Synergy
The efficiency of a plasma-based Beam Processing Center is also measured by its ability to handle material flow. Because plasma cutting is faster than traditional thermal methods, the bottleneck in production often shifts to material handling. However, the non-contact nature of plasma allows for a more streamlined conveyor and gripper system. Since there is no need for high-pressure clamping to resist mechanical cutting forces, the risk of deforming the beam flanges is eliminated.
The plasma system’s ability to “mark” the steel—using a lower amperage setting to etch part numbers or layout lines—further enhances the efficiency of the center. This integrated marking, performed by the same torch head used for cutting, ensures that every piece of steel leaving the BPC is ready for immediate assembly. The industrial engineer sees this as a reduction in “Work in Progress” (WIP) and an increase in overall floor space utility.
Technical Integration of G-Code and Plasma Parameters
The software layer of the BPC translates 3D CAD models into G-code that includes specific plasma parameters. These parameters include gas pressures (typically oxygen or nitrogen), arc current, and the AVC voltage setpoints. For an H-beam with varying flange thicknesses, the software can dynamically adjust the cutting speed and amperage.
This digital integration ensures that the intersection accuracy is maintained even when the geometry becomes complex. For instance, when the torch moves from a thick flange to a thinner web, the AVC and the power source work in tandem to prevent over-burn. This level of control is what allows plasma-based BPCs to achieve “bolt-ready” quality directly from the machine, significantly reducing the total cost of ownership (TCO) for structural steel fabricators.
Conclusion on Process Optimization
In summary, the application of plasma cutting within a Beam Processing Center, underpinned by robust Arc Voltage Control, represents the pinnacle of current structural steel fabrication technology. By focusing on the precision of the arc and the flexibility of robotic motion, fabricators can achieve unparalleled accuracy in intersections and bevels. The inherent low-maintenance characteristics of the plasma process, combined with its ability to handle the rugged realities of H-beam production, make it an indispensable tool for the modern industrial engineer looking to maximize throughput without sacrificing quality.






