H-Beam Production Line with 3D Vision positioning for LNG Projects
In this article
Optimizing LNG Structural Fabrication via 3D Vision Plasma Systems
Liquefied Natural Gas (LNG) projects demand an unprecedented level of structural integrity due to the cryogenic temperatures and volatile environments involved. The primary skeleton of these facilities relies heavily on H-beam structures, which must be fabricated with extreme precision to ensure load-bearing capacity and seismic resilience. Traditional fabrication methods often struggle with the inherent irregularities of hot-rolled steel. The introduction of 3D vision positioning in Plasma Cutting lines addresses these variances by bridging the gap between theoretical design and physical reality.
Industrial engineers are now prioritizing automated plasma lines that utilize high-definition scanning to map the H-beam surface before a single arc is struck. This approach eliminates the cumulative error typically found in manual layout processes. In the context of LNG modules, where thousands of beams must interlock perfectly, the ability to compensate for beam camber, sweep, and flange tilt is not just an efficiency gain; it is a fundamental requirement for structural certification.
The Role of 3D Vision in Dimensional Variance Compensation
Hot-rolled H-beams are rarely perfectly straight. Standard manufacturing tolerances allow for slight deviations in web centering and flange parallelism. In high-stakes LNG infrastructure, these deviations can lead to significant fit-up issues during site assembly. A 3D vision positioning system utilizes structured light or laser triangulation sensors to create a high-density point cloud of the beam. This digital twin is then compared against the original Building Information Modeling (BIM) data.
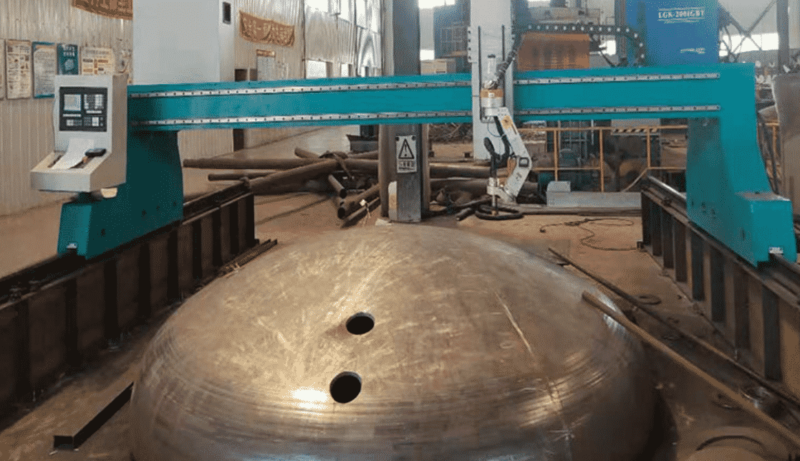
The system automatically shifts the cutting path in real-time to align with the actual physical center of the beam rather than the theoretical center. This ensure that bolt holes, cope cuts, and intersections are placed with sub-millimeter accuracy. For engineers, this means the end-product maintains its designed center-of-gravity and load distribution, regardless of the mill-source irregularities of the raw steel.
Precision Plasma Cutting and Intersection Accuracy
In LNG pipe racks, H-beams often serve as the primary support for complex piping networks. This requires intricate intersection cuts where secondary beams or pipe supports pass through or join the main structural members. Plasma cutting technology, when integrated with a 6-axis robotic arm, allows for complex geometries that were previously labor-intensive or impossible to achieve with mechanical means.
Intersection accuracy is critical because gaps larger than 2mm can significantly weaken a joint or require excessive filler material during subsequent stages. Robotic plasma torches, guided by 3D vision, can execute “mouse-hole” cuts, rat-holes, and circular penetrations with high-speed thermal precision. The plasma arc remains perpendicular to the cutting surface or tilts according to the programmed bevel, ensuring that the internal faces of the cuts are clean and require minimal grinding. This level of accuracy reduces the “re-work” rate, which is a key performance indicator in large-scale energy projects.
Advanced Beveling for High-Strength Joints
Welding requirements for LNG structures are governed by strict codes such as AWS D1.1 or Eurocode 3. To meet these standards, H-beams must often feature complex bevels—V, Y, K, or X profiles—to allow for full penetration. Manual beveling is inconsistent and slow. A robotic plasma system, however, can perform multi-pass beveling in a single sequence.
By utilizing the 3D scan data, the robot adjusts its torch angle to compensate for any flange warping. This ensures a consistent root face and bevel angle across the entire length of the cut. This consistency is vital for automated welding processes that may follow, as it allows for uniform heat input and predictable weld pool behavior. The precision of the plasma cutting beveling ensures that the structural joint can withstand the thermal contraction cycles inherent in LNG processing environments.
Low Maintenance Profiles for Industrial Throughput
From an operational standpoint, the longevity of a production line is as important as its precision. Robotic plasma systems are designed for high duty cycles with H-beam low maintenance requirements. Unlike mechanical drilling or sawing systems, plasma cutting is a non-contact process. There is no tool wear, no broken drill bits, and no coolant management required. This significantly reduces the overhead cost per ton of fabricated steel.
Modern plasma power sources use long-life electrode technology and silver-contact consumables that extend the interval between maintenance shutdowns. Furthermore, the absence of massive mechanical forces during cutting means the structural frame of the machine does not suffer from vibration-induced fatigue. This stability ensures that the 3D vision sensors remain calibrated for longer periods, maintaining the system’s accuracy over years of operation in harsh industrial climates.
Integration with Material Handling and ERP
The efficiency of an H-beam line is maximized when the 3D vision system communicates directly with the factory’s ERP. As the beam enters the cutting zone, its unique ID is scanned, and the corresponding NC (Numerical Control) files are loaded. The vision system confirms the material length and profile type, providing an automated “gatekeeper” function that prevents the processing of incorrect sections. This digital traceability is a mandatory component for many LNG project developers, who require a complete data log for every structural component used in the facility.
Thermal Management and Kerf Compensation
A sophisticated industrial engineer understands that plasma cutting introduces heat into the workpiece. 3D vision systems can be programmed to account for thermal expansion during the cutting process. By sequencing cuts and using intelligent kerf compensation algorithms, the system ensures that the final dimensions of the H-beam are accurate once the material has cooled to ambient temperature. This level of control is particularly important for the long-span beams used in modular LNG construction, where even a 0.1% thermal expansion error can result in a significant misalignment across a 12-meter member.
Summary of Technical Advantages
The synergy between 3D vision positioning and robotic plasma cutting represents the current pinnacle of H-beam fabrication. By focusing on the intersection of software-driven accuracy and robust hardware, LNG project fabricators can achieve a throughput that manual shops cannot match. The reduction in physical tool maintenance, combined with the elimination of layout errors, positions these automated lines as the backbone of modern energy infrastructure manufacturing.
Ultimately, the goal is a “zero-defect” production environment. Through the use of real-time scanning, multi-axis torch movement, and advanced thermal processing, the structural steel industry is now capable of meeting the rigorous demands of the global LNG market with high efficiency and uncompromising safety standards.






