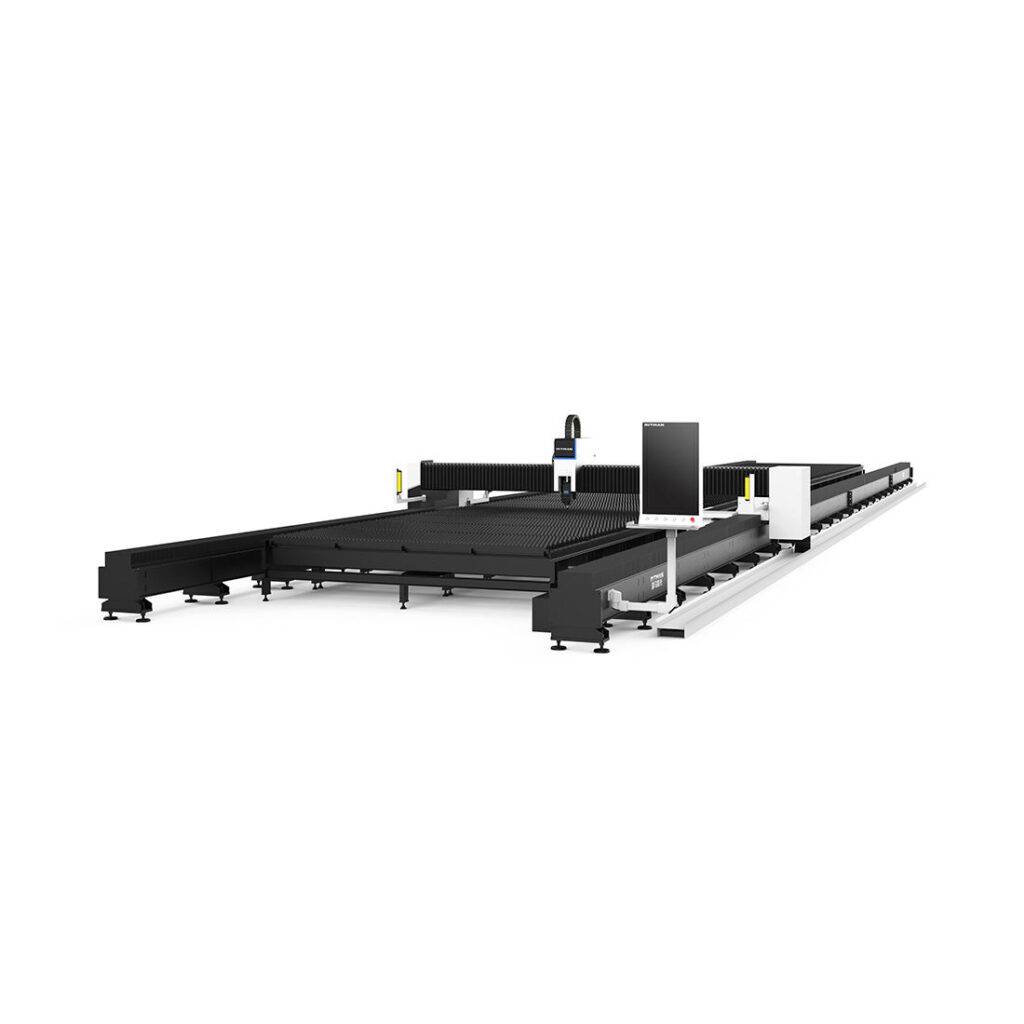
Fiber Laser Cutting Machine with Laser Seam Tracking for Steel Structure
In this article
- Optimizing Structural Steel Fabrication via Fiber Laser Technology
- The Role of Laser Seam Tracking in Precision Cutting
- Consolidated Processing: Punching, Marking, and Cutting
- Eliminating Post-Processing: The No-Grinding Mandate
- Technical Specifications and Performance Metrics
- Conclusion: The Engineering ROI
Optimizing Structural Steel Fabrication via Fiber Laser Technology
In the current landscape of industrial manufacturing, the transition from traditional mechanical processing to Fiber Laser Cutting Machine technology represents a significant leap in throughput and precision. Structural steel fabrication—characterized by heavy-duty I-beams, H-beams, and large plate assemblies—demands a level of accuracy that minimizes cumulative error. Fiber lasers, operating at a wavelength of approximately 1.07 microns, offer a beam quality that allows for extremely high power density. This focusability ensures that the energy is concentrated on a minute spot, resulting in a narrow kerf width and a minimal Heat Affected Zone (HAZ).
For the industrial engineer, the objective is the reduction of total cycle time. By leveraging fiber laser systems, the workflow moves from a multi-stage process to a streamlined, single-station operation. The ability to maintain high feed rates on thick carbon steel and stainless steel sections while preserving edge perpendicularity is the primary driver for ROI in modern steel service centers.
The Role of Laser Seam Tracking in Precision Cutting
Structural steel is rarely perfectly flat or straight. Material deviations, such as crowning in beams or surface irregularities in hot-rolled plates, present challenges for high-precision cutting heads. This is where Laser Seam Tracking becomes an essential component. Unlike standard capacitive height sensors that only measure vertical distance, a dedicated laser tracking system utilizes optical triangulation or specialized sensors to map the topography of the workpiece in real-time.
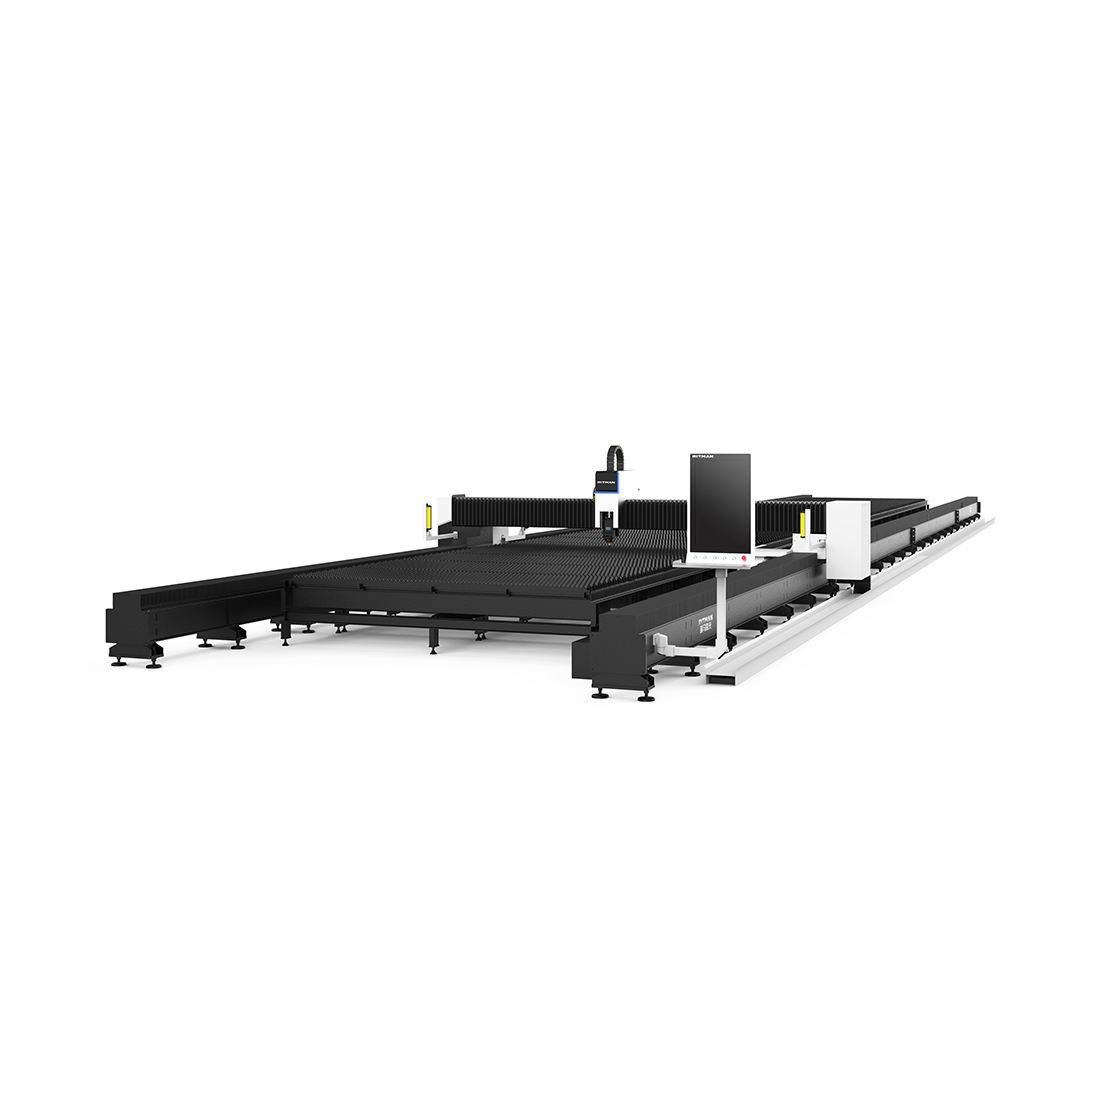
This system compensates for material deformation and positioning errors by dynamically adjusting the cutting path. In large-scale steel structures, even a three-millimeter deviation over a twelve-meter beam can lead to assembly failures. Seam tracking ensures that the laser nozzle remains perfectly aligned with the programmed geometry, regardless of the physical inconsistencies of the raw material. This capability is critical for complex geometries such as cope cuts, bolt holes, and interlocking tabs that require high-tolerance fit-ups.
Consolidated Processing: Punching, Marking, and Cutting
One of the most significant advantages of a fiber laser system in Structural Steel Fabrication is the consolidation of three distinct operations: punching, marking, and cutting. Traditionally, these tasks required separate machines, increasing material handling time and the risk of dimensional drift.
High-Speed Punching Simulation
While mechanical punching is limited by die wear and material thickness, the fiber laser “punches” holes by executing high-speed circular interpolations. The result is a hole with no mechanical deformation of the surrounding material, a common issue with hydraulic punches. This is vital for structural integrity, as it prevents micro-cracking around bolt holes that could lead to fatigue failure.
Integrated Part Marking
Traceability is a non-negotiable requirement in modern construction. Fiber lasers can be modulated to perform low-power surface etching or marking. This allows for part numbers, QR codes, and assembly orientation lines to be etched directly onto the steel surface during the cutting cycle. Because the marking is done in the same coordinate system as the cut, the placement is accurate to within microns.
Precision Cutting and Edge Quality
The final cut produced by a fiber laser is characterized by a smooth surface finish. The high-frequency pulse capability of the laser source allows for fine control over the melt pool. This leads to a dross-free edge that complies with high-level structural standards, such as those required for bridge components or high-rise skeletons.
Eliminating Post-Processing: The No-Grinding Mandate
From an industrial engineering perspective, grinding is a “non-value-added” activity. It introduces labor costs, consumes abrasives, and creates hazardous dust environments. A primary goal of implementing a high-precision fiber laser is the total elimination of secondary grinding.
Because the fiber laser utilizes a high-pressure assist gas (typically Oxygen for carbon steel or Nitrogen for stainless steel), the molten material is ejected cleanly from the Kerf Management zone. The resulting edge is clean, square, and ready for immediate assembly or surface treatment. In structural applications where coatings or galvanization are required, the absence of oxide layers (when using nitrogen) or the consistency of the oxide layer (when using oxygen) ensures superior coating adhesion. This “cut-and-ship” capability drastically reduces the footprint of the fabrication shop and shortens lead times.
Technical Specifications and Performance Metrics
To maximize the efficiency of a fiber laser in steel structures, several technical parameters must be harmonized:
Beam Parameter Product (BPP)
A lower BPP indicates a beam that can be focused to a smaller spot size over a longer distance. For structural steel, where thick sections are common, maintaining a consistent beam waist throughout the material thickness is essential for ensuring the cut is square and not tapered.
Dynamic Motion Control
The gantry systems housing the laser head must support high acceleration and deceleration rates. When the laser seam tracking detects a deviation, the motion control system must respond with zero latency to correct the path. This requires high-torque servo motors and rigid mechanical frames to prevent vibration from translating into the cut surface.
Thermal Management
Structural steel absorbs heat. Advanced fiber lasers utilize sophisticated nesting software that calculates thermal distribution, ensuring that the laser does not dwell in one area for too long, which would otherwise cause thermal expansion and dimensional inaccuracies.
Conclusion: The Engineering ROI
Integrating a fiber laser cutting machine with Laser Seam Tracking into a structural steel workflow is an investment in process stability. By removing the variables associated with manual layout, mechanical punching, and manual grinding, the facility moves toward a predictable, data-driven production model. The precision afforded by these systems ensures that every component fits perfectly during site erection, reducing the need for costly field modifications. In the competitive landscape of steel fabrication, the ability to deliver high-precision, multi-functional processing with minimal labor intervention is the ultimate hallmark of modern industrial efficiency.






